

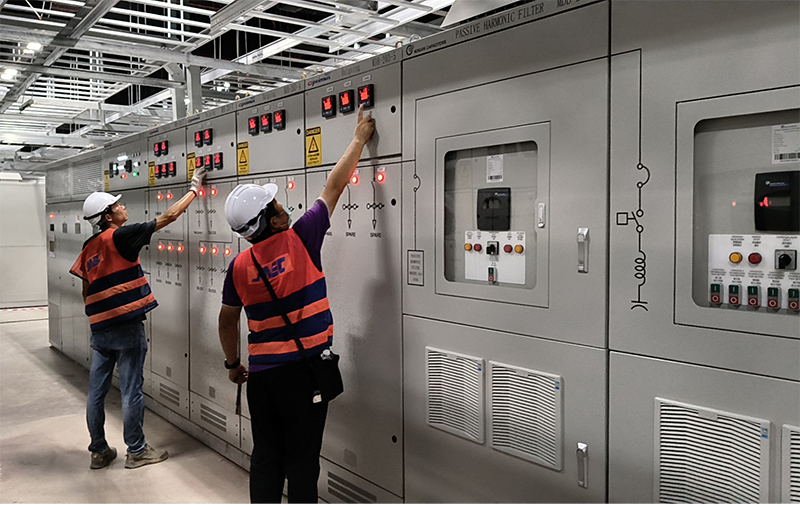
在 EPC 工程总承包模式下,配电系统分包的交付质量与进度,直接影响整体项目的节点履约与验收成本。很多项目的配电分包风险,往往到现场安装、调试验收阶段才集中暴露:货不对板导致性能不达标、尺寸偏差导致现场返工、产能脱节导致工期延误,既增加项目成本,也消耗总包方的协调精力。事实上,绝大多数现场风险,都可以通过出厂前的系统化管控前置化解。 Under the EPC (Engineering, Procurement and Construction) general contracting model, the delivery quality and schedule of power distribution system subcontracts directly affect milestone performance and acceptance costs of the overall project. Risks of power distribution subcontracts in many projects are often fully exposed only during on-site installation, commissioning and acceptance: mismatched goods resulting in substandard performance, dimensional deviations causing on-site rework, and disconnection in production capacity leading to schedule delays. These problems not only raise project costs but also consume coordination efforts of the general contractor. In fact, most on-site risks can be resolved in advance through systematic pre-delivery control.
一、配电分包三大现场高发风险 Three High-Frequency On-site Risks of Power Distribution Subcontracts
1.货不对板,性能偏差Mismatched Goods and Performance Deviation
部分分包方交付产品存在导体材质降级、绝缘工艺缩水、元器件参数偏差等问题,与技术协议要求不符。这类问题隐蔽性强,往往到现场试验、竣工验收阶段才被发现,返工周期长、整改成本高,严重时直接影响项目整体验收。 Some subcontractors deliver products with degraded conductor materials, compromised insulation processes, and component parameter deviations, which fail to meet the requirements of the technical agreement. Such defects are highly concealed and usually detected only during on-site tests and final acceptance. They involve long rework cycles and high rectification costs, and in severe cases, directly affect overall project acceptance.
2.接口错配,现场返工Mismatched Interfaces and On-site Rework
配电产品尺寸偏差、接口标准不统一、插接配合度不足,是现场高频问题。为适配现场工况进行切割、改制、补焊,不仅打乱施工节奏,还会破坏原有结构与防护性能,留下长期运行隐患。 Dimensional deviations, inconsistent interface standards and poor plug-in fit of power distribution products are frequent on-site issues. Cutting, modification and repair welding to adapt to site working conditions will not only disrupt construction schedules, but also damage the original structure and protection performance, leaving hidden dangers for long-term operation.
3.排产失准,工期延误 Inaccurate Production Scheduling and Schedule Delay
供应商产能评估不足、生产节点失控、物流协同脱节,导致交付滞后于项目施工计划,进而影响电缆敷设、设备安装、系统调试等后续工序,甚至触发整体项目的工期违约风险。 Insufficient capacity assessment, out-of-control production milestones and disconnected logistics coordination by suppliers cause delivery delays against project construction plans. This will affect subsequent procedures including cable laying, equipment installation and system commissioning, and may even trigger liquidated damages risks for the whole project.
二、全流程出厂管控,把风险闭环在工厂内Full-process Pre-delivery Control: Closing Risk Loop Within Factory
风险前置是成本最低的管控方式。美嘉科技建立从原材料、生产、检测到出厂的全流程管控体系,将质量、尺寸、工期三类核心风险最大限度控制在出厂前,减少现场不确定性。 Risk pre-control represents the most cost-effective management method. Mega Technology has established a full-process control system covering raw materials, production, inspection and shipment. It maximizes control over three core risks: quality, dimension and schedule before delivery to reduce on-site uncertainties.
三级品控体系:从源头锁定材质与工艺Three-level Quality Control System: Locking Materials and Processes from the Source
建立 “原材料进厂检 - 制程节点检 - 成品终检” 三级品控机制,全链路对标技术协议要求: A three-level quality control mechanism of "raw material incoming inspection - in-process milestone inspection - finished product final inspection" is established, with the whole chain aligned with technical agreement requirements:
・原材料端:导体、绝缘材料、柜体板材逐批核验规格、材质证明与关键参数,核心物料批次可追溯,从源头杜绝材质降级; ・Raw material stage: Specifications, material certificates and key parameters of conductors, insulating materials and cabinet plates are verified batch by batch. Batches of core materials are traceable to eliminate material degradation at source.
・制程端:在绝缘成型、柜体焊接、元器件装配等关键工序设置质控卡点,严格按工艺标准作业,每道工序合格后方可流入下一环; ・Production stage: Quality checkpoints are set for key processes such as insulation forming, cabinet welding and component assembly. Operations are performed in strict accordance with process standards, and each process can only proceed to the next after passing inspection.
・成品端:每批产品完成后,逐项完成电气性能、机械尺寸、外观防护全项检验,确保成品与设计要求一致。 ・Finished product stage: After each batch is completed, comprehensive inspections on electrical performance, mechanical dimensions and surface protection are carried out item by item to ensure finished products comply with design requirements.
出厂预组装验证:前置消解接口安装风险 Pre-assembly Verification Before Shipment: Eliminating Interface Installation Risks in Advance
针对模块化母线、成套柜体等产品,出厂前完成分段预组装与接口适配校验,核对安装尺寸、连接公差、插接配合度,验证现场拼接的可行性与匹配度。提前发现尺寸偏差、接口不匹配问题并在厂内整改,确保现场可直接对接安装,避免现场切割改制带来的返工与质量隐患。 For products such as modular busbars and complete cabinet sets, sectional pre-assembly and interface adaptation verification are completed before shipment. Installation dimensions, connection tolerances and plug-in fit are checked to verify the feasibility and matching of on-site splicing. Dimensional deviations and interface mismatches are identified and rectified in the factory in advance, ensuring direct on-site installation and avoiding rework and quality risks caused by on-site cutting and modification.
Intertek 认证实验室检测:性能数据可追溯 Testing by Intertek-accredited Laboratory: Traceable Performance Data
依托公司 Intertek 认证实验室,可按国标、国际标准完成温升、工频耐压、短路耐受等全项型式试验与出厂抽检。所有检测数据可追溯、报告可核验,产品性能指标与技术协议的一致性可验证,避免现场验收才发现性能不达标,为项目验收提供权威依据。 Relying on the company’s Intertek-accredited laboratory, full type tests and pre-shipment sampling tests including temperature rise, power frequency withstand voltage and short-circuit withstand can be performed in accordance with national and international standards. All test data is traceable and reports are verifiable. Consistency between product performance indicators and technical agreements can be validated, preventing performance non-conformities discovered only at on-site acceptance and providing authoritative support for project acceptance.
标准化厂验机制:出厂前共同把关 Standardized Factory Acceptance Test (FAT) Mechanism: Joint Inspection Before Shipment
建立标准化客户厂验流程,明确厂验检测项、验收标准与判定规则。EPC 总包方可在出厂前赴厂开展现场核验,对照图纸、技术协议逐项核查产品参数、工艺质量与配置清单。所有查验出的问题在厂内整改闭环后再发货,将问题解决在出厂阶段,最大限度降低现场整改成本。 A standardized customer FAT process is formulated with clear test items, acceptance criteria and judgment rules. EPC general contractors may carry out on-site factory inspection before shipment, verifying product parameters, workmanship quality and bill of configuration item by item against drawings and technical agreements. All identified issues are rectified and closed in the factory prior to delivery, resolving problems before shipment and minimizing on-site rectification costs.
订单全周期排产:锁定交付节点 Full-cycle Order Production Scheduling: Securing Delivery Milestones
具备成熟的订单评审与产能排产机制,订单落地即完成产能核算与节点拆解,明确生产、检验、发货各阶段时间点,全程同步项目进度。核心工序标准化作业、产能稳定可控,可有效规避排产混乱、产能不足导致的工期延误风险,保障交付节奏匹配项目整体施工计划。 We have a mature order review and capacity scheduling mechanism. Once an order is confirmed, capacity calculation and milestone breakdown are completed to define timelines for production, inspection and delivery, synchronizing with project progress throughout the whole cycle. Standardized core processes and stable, controllable production capacity effectively avoid schedule delays caused by chaotic scheduling or insufficient capacity, ensuring delivery rhythm matches the overall project construction plan.
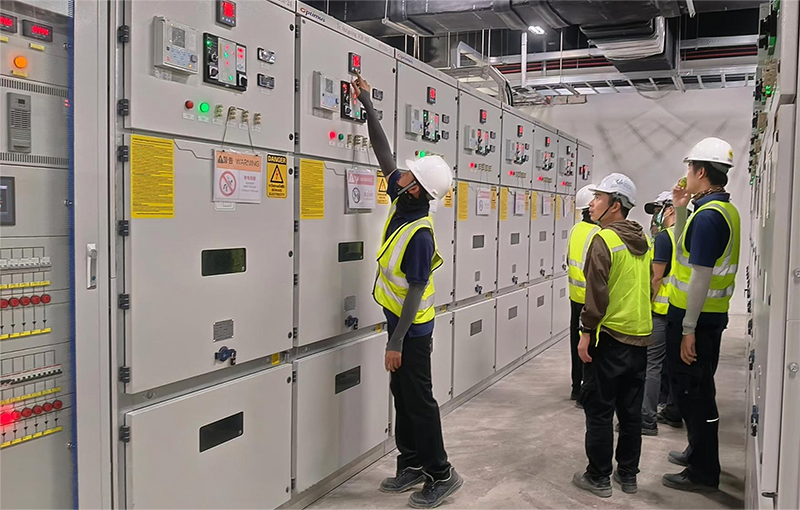
三、出厂前置管控,为 EPC 创造三重价值 Pre-shipment Front-end Control: Three-fold Value for EPC Projects
对于 EPC 总包方而言,将配电分包的管控端口前移至工厂端,核心价值体现在三个方面: 一是降低现场综合成本,减少现场返工、改制与协调成本,避免工期延误带来的窝工损失与违约风险; 二是简化验收闭环流程,原厂检测资料齐全,性能参数可验证,降低验收沟通成本与反复整改的时间消耗; 三是厘清质量责任边界,出厂前明确产品质量状态,避免现场问题出现后的责任界定纠纷。 For EPC general contractors, shifting the control boundary of power distribution subcontracts to the factory side delivers three core values: First, reduce overall on-site costs, cut expenses for on-site rework, modification and coordination, and prevent idle work losses and default risks caused by schedule delays. Second, simplify acceptance closure procedures. Complete original factory test documents and verifiable performance parameters lower communication costs for acceptance and time spent on repeated rectification. Third, clarify quality responsibility boundaries. Product quality status is confirmed before shipment to avoid disputes over liability when on-site defects occur.
优质的配电分包,从来不是 “货到现场再说”,而是从生产端就开始的风险共担与过程可控。美嘉科技依托全流程品控体系、第三方认证检测能力与标准化交付机制,将配电分包的质量、进度风险最大限度控制在出厂前,助力 EPC 项目实现品质可控、工期可控、成本可控。 High-quality power distribution subcontracting is never a "ship first and deal with issues on site" model. Instead, it features shared risks and process controllability starting from production. Supported by the full-process quality control system, third-party accredited testing capability and standardized delivery mechanism, Mega Technology maximizes containment of quality and schedule risks of power distribution subcontracts before shipment, helping EPC projects achieve controllable quality, schedule and cost.
如果您有 EPC 项目配电分包需求,欢迎对接咨询,我们将提供从方案配合到出厂交付的全流程支持。 If you have requirements for power distribution subcontracts for EPC projects, please feel free to contact us for consultation. We provide full-cycle support from solution coordination to pre-shipment delivery.
